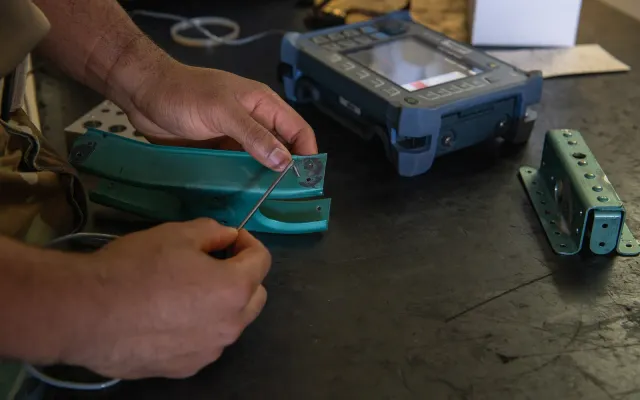
Ultrasonic thickness testing measures wall thickness at one spot by timing a sound pulse through the steel and back. The gauge knows the speed of sound in the material, halves the round-trip time and shows a number. On a tank shell, an elbow or a suspect area on a joint, that number is fast and accurate. On a whole string of tubing it tells you about the few square inches under the probe and nothing about the rest. Corrosion pits and rod wear are local, so a UT spot check can read full wall on a joint that has a groove a foot away. That’s the main reason tubing gets scanned full length with electromagnetic inspection (EMI) and UT gets used to put a number on specific spots.
How ultrasonic thickness testing works
Evident, which makes thickness gauges, gives the formula as T = V × (t/2). T is thickness, V is the velocity of sound in the material and t is the measured round-trip transit time. The pulse goes in, bounces off the far wall and comes back, so the gauge divides the time by two. The transit time is usually a few millionths of a second.
In the field that formula means three things.
- The velocity setting has to match the steel. Evident says sound velocity changes from material to material and “can change significantly with temperature,” so the gauge has to be calibrated to the material being measured. A reading is only as good as that calibration.
- Sound needs a couplant. Megahertz sound doesn’t cross an air gap, so a drop of gel, glycerin, propylene glycol, water or oil goes between the probe and the steel.
- One side is enough. Pulse-echo UT needs access from one side only, according to Iowa State’s NDE-Ed course material. That’s why it works on a closed vessel or a joint you can’t see inside.
Wikipedia’s entry on ultrasonic thickness measurement lists 5 MHz as a standard gauge frequency and puts good accuracy at 0.1 mm or better with standard timing.
Corrosion gauges vs precision gauges
Gauges come in two families. Corrosion gauges use dual-element transducers: separate send and receive crystals angled to focus just under the surface. Evident calls remaining wall on corroded pipes, tanks and vessels “the single most important application” for ultrasonic gauging. Duals are built to find the minimum remaining thickness on a rough, pitted surface. They give up some accuracy to do it.
Precision gauges use single-element probes. Evident says they can read to ±0.001 in. (0.025 mm) on smooth material, which a corrosion gauge can’t match.
For oilfield equipment that has seen produced fluid, you almost always want the corrosion gauge, because what you need to know is the thinnest wall left.
Gauges also differ in what they time. Mode 1 times from the pulse to the first back-wall echo and is the general-purpose setting. Mode 3 times between two back-wall echoes. Evident says Mode 3 gives the best accuracy and thin-wall resolution, but only on material that returns clean multiple echoes. Corroded inside walls often don’t.
What throws a UT reading off on location
Most bad UT numbers come from setup and surface conditions, not the instrument. ASNT lists surface preparation, couplant, complex geometry and operator training among the method’s limits. NDE-Ed adds that rough, irregular or very thin material is hard to inspect, and that reference standards are needed for calibration.
| Problem | What happens | What to do |
|---|---|---|
| Wrong velocity setting | Every reading is off by the same percentage | Calibrate on a block of known thickness in the same steel |
| Hot steel | Velocity shifts. Most contact probes are rated to about 125°F (50°C), and hotter surfaces can damage them | Check surface temperature first. Use high-temperature duals or delay lines on hot pipe |
| Small diameter | Coupling falls off on a tight curve | Use a smaller probe face |
| Paint, liner or coating | The gauge can read coating plus steel, or misread the interface echo | Use a mode or setup made for coated steel, or strip a spot |
| Scale, rust or dry couplant | Weak or no back-wall echo | Clean to bare metal and recouple |
| Pitting on the far side | The probe lands between pits and reads full wall | Take a grid of readings, or scan first |
The 125°F limit matters in the Permian. NOAA’s 1991-2020 normals for Midland International Airport put average daily highs at 95.0°F in June, 95.8°F in July and 94.8°F in August. That’s the air temperature. Dark steel sitting on a pipe rack in full sun runs hotter than the air, so check the surface before you trust a contact probe in summer.
Ultrasonic pipe thickness testing vs EMI on tubing
On a single spot, UT is hard to beat. Over a few hundred joints, coverage becomes the problem. A pit or a rod-wear groove covers a small part of the wall. A spot reading only finds it if the probe happens to land on it.
| Ultrasonic thickness testing | EMI tubing inspection | |
|---|---|---|
| What it measures | Wall thickness under the probe | Wall loss and defects along each joint |
| Coverage | Points, or a grid you lay out | Full length of every joint scanned |
| Surface prep | Clean contact surface plus couplant | Non-contact |
| Finds rod wear on the inside wall | Only where a reading lands on the groove | Yes, along the joint |
| Output | A thickness number per point | A trace or grade per joint |
| Best use | Proving up a known spot, vessels, surface piping, fittings | Grading a pulled string joint by joint |
Rod wear is a good example. Rod wear usually sits on one side of the wall. A UT reading 90 degrees around from the wear reads full wall. Rod pump tubing wear walks through where that wear shows up and why it’s local.
This matches how the pipe is made. IOGP’s supplementary specification to API 5CT, which oil companies use when buying casing and tubing, requires wall thickness to be measured and recorded over the full length for several grades. Some grades need 100% of the surface covered by an automated system. If the mill doesn’t trust spot checks on new pipe, a few spot readings on used pipe that has seen produced water won’t tell you much about the whole string.
What a reading means: the 12.5% tolerance
A thin reading doesn’t always mean corrosion. The same IOGP specification sets the permitted under-tolerance on tubing wall at 12.5%, so new pipe can come out of the mill thinner than its nominal wall. The purchaser can ask for a tighter tolerance of -10%, -7.5% or -5%.
Here’s the arithmetic for a tube specified at 0.217 in. of wall:
- 0.217 × 0.875 = 0.190 in.
- A brand-new joint could legally read 0.190 in. at its thinnest point.
- A used joint reading 0.195 in. may have lost almost nothing.
So a UT number means little without the specified wall, the tolerance and a baseline reading from the same spot. Grading used tubing needs the nominal wall and a remaining-wall criterion your operator or engineer has set. A single reading taken without that context isn’t a pass or a fail.
When UT is the right tool
UT fits when:
- You need a number on a known spot. A scan or a visual check found something, and you want the remaining wall in thousandths.
- The item isn’t tubing on a rack. Tank shells, separators, surface flowlines, elbows and tees are UT jobs.
- You’re tracking a fixed point over time. Mark the location, read it at the same spot each visit and the trend is real.
- You only have one side, such as a closed vessel or a buried line with one excavated spot.
Use a full-length scan when the question is “which of these joints can go back in the hole.” That covers a pulled string after a rod job, a well with a corrosion history, or a CO2 producer.
Who should take the readings
ASNT notes that UT requires a high level of expertise and offers Level II and Level III certification. Wikipedia notes that ship classification societies expect thickness-measurement operators to hold Level II under ASNT’s SNT-TC-1A or an equivalent scheme. If a UT report is going to decide whether equipment stays in service, ask who took the readings, how the gauge was calibrated and which block was used.
Full-length tubing inspection in the Permian
Site Safe Solutions provides EMI tubing inspection in the Permian Basin. Non-contact electromagnetic scanning finds wall loss, rod wear, corrosion and other defects in tubing, and each job leaves digital trace records. If you have a string coming out on a workover and want to know which joints can be rerun, tell us the well and the pull date. For what the scan picks up, see what EMI tubing inspection finds.